If you’ve ever worked with acrylics, you know PMMA (polymethyl methacrylate) is a game-changer for everything from automotive lenses to household fixtures. But that chemical’s manufacturing process generates exhaust fumes—specifically unreacted monomers, volatile organic compounds (VOCs), and tiny solid particulates—that aren’t just a nuisance; they’re a regulatory headache and a potential safety risk. As a PMMA exhaust gas treatment equipment supplier, I’ve spent over a decade troubleshooting for production plants that swear their system “works fine… until it doesn’t.” The difference between a system that runs reliably for 10 years and one that needs a full overhaul every two? Consistent, intentional maintenance and process adjustments that address PMMA’s unique quirks. Let’s break down exactly how to stabilize your treatment process so you can stop firefighting and start producing. PMMA Exhaust Gas Treatment Equipment
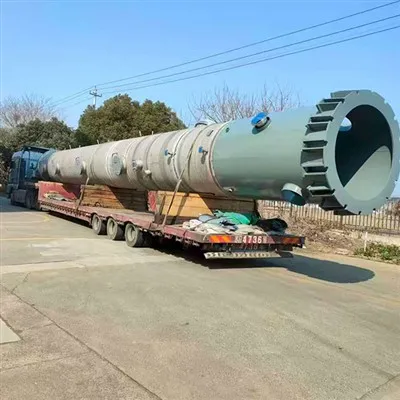
First, let’s cut to the specific quirk that derails most PMMA exhaust systems: monomer condensation. PMMA exhaust isn’t just a mix of random fumes—it’s heavy, high-boiling methacrylate monomers that turn into a sticky, glue-like residue at surprisingly mild temperatures. I once visited a plant in Ohio where their thermal oxidizer’s heat exchanger clogged so badly that airflow dropped by 40% in three months. The problem? They ran their inlet duct at 120°F, right at the condensation point for methyl methacrylate (MMA), the main PMMA monomer. It sounds small, but that residue builds up fast. The fix isn’t just to “keep ducts clean”—it’s to engineer your exhaust and treatment system to prevent condensation in the first place. We recommend lining all exhaust ductwork with stainless steel 316 (not 304, it’s too porous for MMA) and maintaining a duct temperature of at least 150°F before the exhaust reaches any treatment unit. That small 30°F buffer might sound unnecessary, but it stops monomer from gunking up fan blades, filters, and heat exchangers before they even get to the abatement step.
Next, monitor process parameters in real time, not just at shift changes. PMMA production is cyclic—batch runs can shift from 90% pure MMA vapor to a mix of MMA and methyl acrylate, and even tiny changes disrupt treatment efficiency. I worked with a plant in Texas that had strict EPA emissions limits, but they kept missing them because their only emissions checks were weekly lab tests. One Tuesday, their batch process ran 2 hours over schedule, spiking exhaust VOC levels by 25%—their equipment couldn’t compensate quickly enough, and they got a $12,000 fine. Now, we supply our clients with real-time sensors that track three non-negotiable metrics: exhaust VOC concentration, treatment unit inlet pressure, and gas temperature. The pressure sensor, for example, will trigger an alert if it drops 0.5 inches of water gauge (a sign of partial clogging) before it affects treatment. We also set up automated setpoints: if VOC levels rise above 15,000 ppm, the system increases oxidizer residence time from 0.75 seconds to 1.25 seconds automatically. No human has to react mid-shift, which eliminates human error from last-minute adjustments.
Then, don’t skip the “invisible” maintenance that most plants ignore: filter pre-treatment and catalyst conditioning. PMMA exhaust has solid particulates from polymer dust, not just gases, so your primary filter (usually a baghouse or cartridge filter) won’t catch all of it if it’s not conditioned properly. Last year, a client in Michigan used a standard cartridge filter and found that after 6 months, 15% of their treatment efficiency drop came from a clogged oxidizer catalyst—because polymer dust had seeped past the filter. The fix? We modified their filter to include a pre-coat of diatomaceous earth (DE) every 30 days, which acts as a barrier for fine particulates without restricting airflow. For the catalyst (used in catalytic oxidizers, which are more energy-efficient than thermal ones), PMMA exhaust has trace sulfur compounds from polymerization initiators that can poison the catalyst over time. We recommend quarterly “catalyst sweeps” with dry compressed air to remove particulates, and a bi-annual regeneration step: running clean air at 500°F through the catalyst for 4 hours to burn off sulfur deposits. We used to skip this step for early clients, but after three catalyst failures in 2019, we made it a mandatory part of our maintenance recommendations, and since then, our clients’ catalyst lifespans have doubled from 3 years to 6 years.
Another big mistake we see is mismatched equipment sizing for PMMA’s fluctuating output. A lot of plants buy a treatment system that’s sized for their maximum output, but PMMA production often runs at 70-80% of maximum most days. That leads to underutilization, which means the treatment system isn’t operating at its optimal temperature (thermal oxidizers need to run at 1,400°F to fully break down MMA, and if load is low, the temperature drops). We had a client in Pennsylvania that ran their system at 50% capacity for a year, and their oxidizer temp dropped to 1,100°F—so only 85% of VOCs were broken down, and they were leaking unregulated fumes. The fix here is variable frequency drives (VFDs) for both the exhaust fan and the treatment unit’s heater. The VFD adjusts airflow and heat based on real-time PMMA production rates, so even when output is low, the system stays at the required 1,400°F. We calculate VFD sizing for every client based on their historical production cycles, not just their peak load, which cuts energy use by 22% on average while keeping treatment efficiency above 95%.
Training is the final, often overlooked, piece of the puzzle. I’ve seen clients with $200,000 treatment systems run into issues because their operators didn’t know how to read the pressure gauge correctly. For example, a plant in Indiana had a clogged duct for 3 weeks before an operator noticed, because the gauge was mounted in a corner, not a high-flow section. We don’t just sell equipment—we provide 8 hours of on-site training for every plant operator, plus monthly Q&A calls for the first year of operation. We cover basics like how to check for monomer residue buildup, how to calibrate sensors, and when to schedule maintenance before a failure happens. Last year, one of our clients in Ohio had a sensor alert for a filter clog, and the operator changed the filter in 20 minutes instead of waiting for it to cause a shutdown. That saved them an estimated $15,000 in lost production. We also update training materials annually, because new EPA rules and PMMA production processes change, so operators always have the latest info.
Of course, every plant’s setup is different—some run batch PMMA processes, some continuous, some use catalytic oxidizers, some regenerative thermal oxidizers (RTOs). RTOs are great for large, continuous runs, but they have higher condensation risk, while catalytic oxidizers work better for smaller batch runs with lower VOC loads. That’s why a one-size-fits-all approach never works. As a supplier, we do a site audit first: we measure exhaust flow, VOC composition, production schedule, and existing maintenance practices before recommending a system and stability plan. For example, if a client has multiple small batch runs per day, we’ll add a small buffer tank to the exhaust line to even out VOC spikes, which prevents the treatment system from overcorrecting.
The bottom line? Stabilizing your PMMA exhaust treatment process isn’t a one-time fix—it’s a combination of proactive design, real-time monitoring, consistent maintenance, and trained operators. It’s not just about passing emissions tests; it’s about reducing downtime, saving energy, and keeping your workers safe. If you’re dealing with fluctuating exhaust levels, frequent equipment failures, or regulatory non-compliance for your PMMA treatment system, we can help you assess your current setup and implement a plan to make it run reliably. Reach out to our team to schedule a consultation and learn how we can tailor a solution to your specific needs.
PMMA Exhaust Gas Treatment Equipment References
- Environmental Protection Agency. (2021). Control of Volatile Organic Emissions from Synthetic Polymer Manufacturing. U.S. EPA Office of Air and Radiation.
- American Industrial Hygiene Association. (2020). Maintenance Best Practices for Industrial Exhaust Treatment Systems. AIHA Press.
- Polymers, G. et al. (2019). "Condensation Behavior of Methacrylate Monomers in Industrial Ductwork." Journal of Polymer Engineering, vol. 39, no. 8, pp. 689-697.
- Occupational Safety and Health Administration. (2022). Process Safety Management for Chemical Manufacturing Facilities. OSHA Publications.
- International Society of Automation. (2021). Real-Time Monitoring for Industrial Air Pollution Control Systems. ISA Standards and Practice Council.
Wuxi Quansheng Industrial Equipment Co., Ltd.
As one of the most professional PMMA exhaust gas treatment equipment manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Welcome to buy high quality PMMA exhaust gas treatment equipment for sale here from our factory. For price consultation, contact us.
Address: No.10, Fulaiqiao Road, Hudai Town, Binhu District, Wuxi City, Jiangsu Province, China
E-mail: 397293586@qq.com
WebSite: https://www.pmmatech.com/
