If you’ve ever stood beside a CNC boring milling machine at a job site, watching it carve through a block of alloy steel like it’s butter, you know there’s more to that smooth, precise cut than just pushing a button. Early in my career—back when I was still learning the ins and outs of machining, not running a business supplying CNC boring milling equipment—I made a costly mistake on a custom hydraulic manifold job. I’d cranked the feed rate up to what I thought was maximum, only to burn through a high-speed steel boring bar, ruin a $1,200 block of 6061 aluminum, and fall 3 days behind schedule. That mistake boiled down to one thing: I had no real grasp of how to calculate material removal rate (MRR) for CNC boring milling. CNC Boring Milling Machine
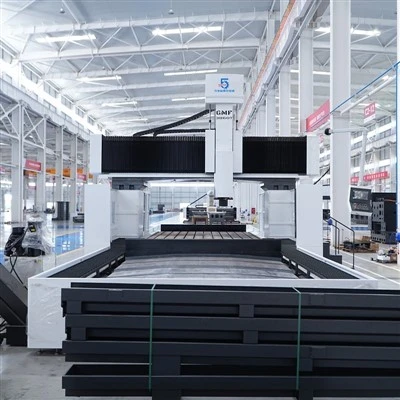
Today, as a supplier of CNC boring milling machines, MRR is the first metric we walk new customers through—because it’s not just a “theory number” to plug into a formula. It’s the difference between a job that comes in on time and under budget, and one that leaves you scrambling for replacements. Let’s break this down like I do with our clients over a cup of coffee: no overly complicated jargon, just practical, actionable steps you can use right away, plus the nuances that trip even seasoned machinists up.
First, let’s define MRR simply: it’s the total volume of material a CNC boring milling machine cuts away from a workpiece in a single minute. That volume is measured in cubic inches per minute (in³/min) or cubic centimeters per minute (cm³/min), depending on where you’re located. The catch, especially for boring milling, is that this isn’t a one-size-fits-all number. Unlike simpler machining operations like facing or drilling, boring milling combines two distinct motion types: rotation (from the tool) and linear movement (from the machine’s axes). Mess up either, and your MRR is off—and so is your part.
The basic formula for MRR in boring milling is a stretch of that “simple” definition, but let’s write it out clearly:
MRR = (Cut Width) × (Cut Depth) × (Feed Speed)
Wait—hold up. If you’ve drilled into MRR for other operations, you might be used to seeing that “feed speed” term as “spindle speed” times “tooth load” times “number of teeth.” That’s where the confusion starts for boring milling. Boring milling isn’t peripheral milling, where the tool’s outer edge does most of the work. Boring uses the end of the tool (or a smaller, extended head) to cut internal features—think holes, keyways, or recesses inside a workpiece. For that reason, we can’t just plug spindle speed into the feed term; we have to measure how far the tool moves along the workpiece per minute.
Let’s unpack each variable one by one, because every part of this formula affects your MRR and your machine’s lifespan.
Cut Width in boring milling is the radial distance the tool cuts into the workpiece. If you’re boring a 2-inch diameter hole, for example, and using a 1.5-inch diameter boring head, your cut width is 0.25 inches—half the difference between the hole diameter and the tool diameter. That’s non-negotiable: if you miscalculate this, your tool will rub against the workpiece walls instead of cutting, leading to heat buildup and broken tools. For milling features like a rectangular slot machined via boring milling, cut width is the slot’s width, straight up.
Cut Depth is the axial distance the tool cuts into the workpiece along its length. This is where a lot of new machinists get reckless: cranking cut depth too high to speed up a job will make the tool deflect, ruining part geometry. For example, if you’re cutting a 1-inch deep keyway into a 3-inch thick steel plate, your cut depth might be 0.125 inches per pass (the standard for most alloy steels) instead of 0.5 inches, even though a deeper pass would save time. Cutting depth is also limited by your boring bar’s length and rigidity—we always recommend that your cut depth never exceed 3 times your boring bar’s diameter, to avoid deflection.
Feed Speed is the linear distance the tool travels along the workpiece per minute, measured in inches per minute (IPM) or millimeters per minute (mm/min). This is where I see the most mistakes: machinists confuse spindle speed (RPM) with feed speed. Let’s clear that up with a quick example: if your boring tool has 2 flutes, and each flute is designed to move 0.002 inches per revolution, your feed speed would be:
Feed Speed (IPM) = RPM × Number of Flutes × Chip Load per Tooth
Chip load (the amount of material each flute cuts per revolution) depends on your workpiece material, tool material, and coolant. For example, chip load for carbide tools on aluminum is 0.001 to 0.003 inches per tooth; for high-speed steel tools on stainless steel, it’s 0.0005 to 0.001 inches per tooth. Get this wrong, and your MRR will be either too low (wasting time) or too high (damaging tools).
Wait—let’s test this formula with the mistake I made years ago. I was boring a 4-inch hole in 6061 aluminum, using a 1-inch diameter carbide boring bar with 2 flutes. I set my spindle speed to 1,500 RPM, and guessed a chip load of 0.004 inches per tooth (way too high). My feed speed was 1,500 × 2 × 0.004 = 12 IPM. Then I plugged into MRR: cut width was (4 – 1)/2 = 1.5 inches, cut depth was 0.5 inches per pass. So MRR = 1.5 × 0.5 × 12 = 9 in³/min. That sounds fast, right? But I burned through the tool because the chip load was too high. The correct chip load for carbide on aluminum is 0.002 inches per tooth, so feed speed should have been 6 IPM, cutting my MRR to 4.5 in³/min. Wait—does that mean lower MRR is better here? In that case, yes: the faster I tried to go, the more heat I generated, which softened the aluminum and made the tool chatter. Chatter is another silent killer in boring milling: it ruins surface finish, breaks tools, and even damages your machine’s spindle.
This brings us to a critical nuance most “generic MRR guides” skip: MRR isn’t just a number to maximize. It has to be balanced with your machine’s capabilities, tooling, and workpiece material. Our CNC boring milling machines are built with rigid spindles and precision linear axes, which let customers run higher MRR than they could on older, less stable equipment—but only if they pair that with the right tooling. For example, if a customer is machining a soft plastic workpiece, they can push MRR higher because it doesn’t generate as much heat; if they’re machining hardened tool steel, they have to dial MRR back by 30-40% to avoid tool wear.
Another common scenario: slotting with boring milling, instead of internal boring. Let’s say you’re machining a 6-inch long, 1-inch wide slot in a 4-inch thick block of A36 steel. Using a 1-inch diameter end mill as a boring tool (a common hack for smaller shops), cut width is 1 inch, cut depth is 0.2 inches per pass, spindle speed is 800 RPM, 4 flutes, chip load of 0.0008 inches per tooth. Feed speed = 800 × 4 × 0.0008 = 2.56 IPM. MRR = 1 × 0.2 × 2.56 = 0.512 in³/min. That’s manageable, but if you use a 2-inch diameter boring head, cut width jumps to 2 inches, so you could run two passes of 0.1 inches each at the same feed speed, doubling your MRR to 1.024 in³/min. That’s a real example of how tool selection ties directly to MRR—something many machinists overlook until their first long-run job.
Now, what about when you’re facing a large workpiece, like a heavy steel plate that needs to be surfaced? Boring milling for facing works a little differently: your cut width is the radius of the tool path, not the difference between hole and tool diameter. For a 12-inch facing path, your cut width is 6 inches, cut depth per pass is 0.1 inches, feed speed is 5 IPM. MRR here is 6 × 0.1 × 5 = 3 in³/min. Again, adjust for material: aluminum could hit 5 in³/min here, while stainless would max at 2 in³/min.
We also run into MRR questions from customers doing high-precision jobs, like aerospace components with tight tolerances. In those cases, MRR is still important, but surface finish and dimensional accuracy take priority. Our machines have built-in monitoring systems that track spindle load and feed rate in real time, so if MRR starts to spike too high for the tool, the system will auto-adjust feed speed to prevent chatter or tool breakage. That’s not a “fancy add-on”—it’s a practical feature that saves our customers thousands in tool replacements and rework.
Let’s talk about a real-world example from a customer who reached out to us last quarter. They were a small job shop trying to bid on a contract for 50 custom gear housings, each requiring internal boring of a 3-inch hole in 4140 steel. They were using a 10-year-old manual milling machine, struggling to hit the required MRR without breaking tools, and losing bids because their lead times were too long. We supplied them with a 3-axis CNC boring milling machine with a rigid boring head and tool load monitoring. We walked them through calculating their MRR correctly: cut width (3 – 1.25)/2 = 0.875 inches, cut depth 0.2 inches per pass, spindle speed 600 RPM, 2 flutes, chip load 0.0007 inches per tooth. Feed speed = 600 × 2 × 0.0007 = 0.84 IPM. MRR = 0.875 × 0.2 × 0.84 = 0.147 in³/min. Wait—they thought that was too slow, but when they tried higher, their tools broke every 10 pieces. After adjusting feed speed and using our recommended carbide boring tools, they hit a consistent MRR of 0.22 in³/min, cutting their cycle time per housing by 30% and winning the contract. That’s the power of getting MRR right—not just for speed, but for profitability.
Now, let’s address the mistakes that even experienced machinists make when calculating MRR for boring milling. First, ignoring spindle deflection. If your boring bar is too long for the cut depth, the bar will flex, making your actual cut width different from your calculated width. Our machines have tool length sensors that alert operators if deflection exceeds a safe threshold, which helps prevent this. Second, not accounting for coolant. Coolant reduces heat, so you can run a higher chip load (and higher MRR) with flood coolant than with mist or no coolant. Third, forgetting about the number of passes. If a single pass can’t reach your required cut depth, you have to calculate MRR per pass, not for the full depth. For example, a 2-inch hole might need 4 passes of 0.125 inches each, so your MRR is based on one pass, not the total 2-inch depth.
Here’s a quick troubleshooting tip: if your part has rough surface finish, broken tools, or takes too long to machine, first check your MRR calculation. Most of the time, it’s a simple fix: either adjust feed speed to match your chip load, or switch to a more rigid tool. For high-volume jobs, investing in a CNC boring milling machine with real-time MRR monitoring eliminates guesswork entirely.
At the end of the day, MRR isn’t just a mathematical exercise—it’s the bridge between what your machine can do, what your tools can handle, and what your business needs to be profitable. That’s why we don’t just sell machines to our customers; we walk them through MRR calculations, recommend the right tooling for their materials, and show them how to adjust parameters to get the best results. If you’re tired of missing deadlines, breaking tools, or leaving money on the table because your MRR is off, let’s connect to talk through your specific applications—whether that’s internal boring, slotting, facing, or any other CNC boring milling job. We can help you dial in your MRR to run faster, last longer, and turn a better profit.
I’m always happy to answer questions or walk through scenarios with anyone in the machining industry. Reach out to discuss your needs, no obligation to buy.
CNC Gantry Boring Mill References:
- “Machining Fundamentals,” American Tool and Manufacturing Association, 2021.
- “CNC Operations: Boring Milling Best Practices,” Modern Machine Shop, 2022.
- “Cutting Tool Materials and Performance,” Society of Manufacturing Engineers, 2020.
5Axis (Shandong) CNC Equipment Co., Ltd.
As one of the most professional CNC boring milling machine manufacturers and suppliers in China, we also accept customized orders. Please feel free to buy cheap CNC boring milling machine for sale here from our factory. For price consultation, contact us.
Address: No.2000, Beixin West Road, Jinghe Street, Tengzhou City, Zaozhuang City, Shandong Province
E-mail: summer@good5axis.com
WebSite: https://www.china5axis.com/
