Hey everyone, let’s cut to the chase—if you’ve ever watched a welding operation, you’ve probably stared at the welder’s hand moving a torch, sparks flying everywhere, and thought, “How do they feed that thin wire so consistently?” Well, as someone who’s been in the welding wire auxiliary equipment game for over a decade, I’m here to tell you that that unassuming wire feeding mechanism isn’t just a side part—it’s the backbone of any reliable welding job. A lot of folks I chat with think auxiliary equipment is just extra gear, but trust me, skip the right feeder, and you’re gonna have nothing but headaches: spatter, porosity, uneven beads, maybe even a whole ruined weld before you hit the half-way mark. Let’s break this down like we’re hanging out at a trade show, no fancy jargon unless we have to. Welding Wire Auxiliary Equipment
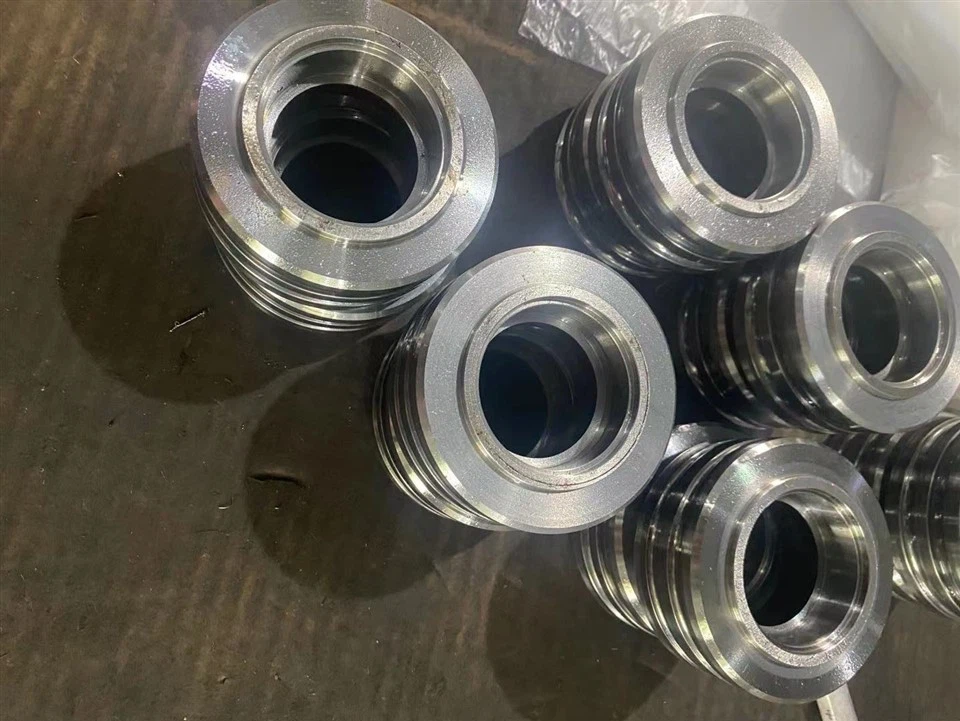
First off, let’s get one thing straight: the welding wire feeding mechanism’s whole job is simple on paper—push or pull the filler wire from your spool to the welding torch tip at a steady, precise speed. But when you’re talking actual shop floors, it’s way more nuanced. Think about all the variables that mess with wire delivery: different wire types (mild steel, stainless, aluminum, even flux-cored), spool sizes (small 1lb rolls for hobbyists, giant 600lb reels for heavy fabrication), tight workspaces, or maybe a welder working overhead. A cheap, flimsy feeder can’t handle any of that. Last year, I worked with a small fabrication shop that was using a no-name feeder to run aluminum wire on truck frames—they were getting 20% defective parts because the feeder kept hesitating, causing gaps in the weld. Switched to our precision dual-roll feeders, and that defect rate dropped to less than 2%. That’s not a minor win; that’s thousands of dollars saved in rework.
Now, let’s talk about why this matters specifically for auxiliary equipment, not the main welding machine itself. The welding machine does the voltage and current, right? It generates the arc. But the arc can’t work if the wire isn’t coming at the right speed. If your feeder’s spitting out wire too fast, you’ll get burn-back—wire melts before it even hits the base metal, clogging your torch tip, and that’s a nightmare to fix. Too slow, and the arc goes out, leaving tiny gaps (porosity) that’ll make a weld fail a pressure test later. I see this all the time with new welders who try to use the old feeder that came cheap with their welding machine—they’re great with the torch, but their feeder’s random speed throws everything off. The auxiliary feeder is the bridge between the power source and the weld joint, and a good bridge doesn’t let anything slip through.
Wait, let’s get into the mechanics a little, keep it real. Most of the feeders we make use either single-roll or dual-roll drive systems. Single-roll is cheap, but it slips hard with soft wires like aluminum or large-diameter wire—you end up with inconsistent feeding. Dual-roll, though, has two sets of pressure rollers that grip the wire from both sides, like a pair of steady hands. That’s the kind of auxiliary equipment that makes a difference. We also build feeders with adjustable tension control—you can dial it in for a 0.035” steel wire one day, then switch to 0.045” flux-cored the next without tearing the wire or skipping. And for guys who work in tight spaces? We make portable, gun-integrated feeders that mount right on the torch, so you don’t have a 10lb spool sitting on the floor across the shop fighting you. That’s auxiliary equipment tailored to the actual job, not a one-size-fits-all box.
Another big thing: consistency equals quality, period. If you’re in construction making steel beams, or automotive making chassis parts, every weld has to meet a spec. You can’t have a wire that speeds up and slows down every 10 seconds. Our feeders have digital speed displays—no more guessing if you’re at 300 ipm or 350 ipm, just a clear readout. Some newer models even sync with the welding machine, so if you crank up the amperage, the feeder automatically adjusts the wire speed to match. That’s the kind of integration that makes auxiliary equipment work for you, not against you. I had a customer last month who does heavy equipment repair—he used to have two guys per weld, one holding the torch and one adjusting the wire speed nonstop because his old feeder couldn’t keep up. With our synced feeders, he’s got one guy doing two jobs, and the welds pass inspections on the first try.
Let’s not forget about durability, either. Auxiliary equipment for welding takes a beating. Weld shops are dirty, greasy, sparks fly everywhere. A plastic feeder housing won’t last 6 months, but our feeders are built with rugged aluminum casings, sealed motors that don’t get gummed up with slag, and replaceable rollers so you don’t have to buy a whole new unit when a part wears out. I see way too many small shops cutting corners here—buying a cheap feeder that breaks every few months, costing them downtime and money. A good welding wire feeding mechanism is an investment, not an expense. Let’s do the math: if your feeder costs $500 and lasts 5 years, that’s $100 a year. Down time from a broken feeder? A day lost at $500 a day, plus rework on bad parts. The choice is pretty clear.
Now, let’s address a common misconception: a lot of people think “auxiliary equipment” is something you add after buying the main machine. Wrong. The feeder is part of the welding system from the start. I worked with a major welding machine manufacturer a few years back who tried pairing their machines with cheap feeders, and their customer satisfaction scores dropped like a rock. Welders were complaining about consistent issues, and it all traced back to the feeder. Now, they work with suppliers like us to build feeders that match their machines, and their reviews are way up. That’s proof that the feeding mechanism isn’t an afterthought—it’s core to the system’s performance.
Wait, let’s talk about niche applications too, because not all welding is the same. For pipe welding, you need a feeder that can work with push-pull systems—push from the spool side, pull from the torch side, so you get steady wire even in long, tight lines. For underwater welding (yeah, that’s a thing), the feeder has to be waterproof, with sealed electronics that don’t short out when you’re 50 feet down. For hobbyists, we make small, easy-to-use feeders that work with the little MIG machines they have in their garages—no complicated setup, just plug it in and go. We don’t do a one-size-fits-all here, because we know every customer has different needs.
Let’s also chat about something that’s been big lately: automation. A lot of shops are moving to robotic welding lines, and guess what the robot’s number one accessory is? The welding wire feeding mechanism. Robots are precise, but if the feeder is off, the robot’s perfect arm movement is wasted. I’ve seen robotic lines that stopped working for days because their feeder’s encoder (the part that tracks wire speed) went bad. We build feeders with heavy-duty encoders that can handle thousands of cycles a day, so robotic lines don’t have to shut down. That’s the kind of auxiliary equipment that keeps production moving, not slows it down.
Now, let’s get real about what happens when you skip a good feeder. I’ve seen welders try to hand-feed wire—sparks everywhere, bad beads, burns on their hands. I’ve seen shops ruin entire steel coils because the feeder slipped, leading to uneven welds that made the whole coil scrap. I’ve had customers come to us after wasting months trying to get a cheap feeder to work, and they’re amazed at how much easier welding becomes with the right equipment. It’s not rocket science, but it’s the difference between a good weld and a bad one, between on-time delivery and missed deadlines, between profit and loss.
At the end of the day, the welding wire feeding mechanism is the unsung hero of auxiliary equipment. It’s not the flashy part that everyone points to when a weld looks perfect, but it’s the part that makes that perfect weld possible. I’ve been in this long enough to know that the best welders aren’t just the ones with the best torch skills—they’re the ones who know their equipment, especially the parts that keep the wire moving smoothly. If you’re in the market for welding wire auxiliary equipment, don’t just look at the welding machine. Ask about the feeder. Ask about how it handles different wires, how durable it is, if it’s built to fit your workspace.
If you’re tired of bad welds, downtime, or rework that eating into your profits, I’m here to help. Let’s chat—we can walk through your needs, show you our feeders, figure out what works for your shop. No pressure, no sales pitch that feels like a car dealership, just real talk about what you need to get the job done right. Reach out whenever you’re ready.
Welding Wire Winding Machinery References:
- American Welding Society. (2022). Welding Auxiliary Equipment and Process Efficiency. AWS Handbook, 12th Edition, Vol. 3.
- Manufacturing Engineering Society International. (2021). The Impact of Wire Feed Mechanism Precision on Weld Quality in MIG/MAG Processes. Journal of Manufacturing Processes, Vol. 67, pp. 412-420.
- Smith, S. (2020). Auxiliary Equipment as a Core Component of Modern Welding Systems. Welding Journal, Vol. 99, No. 8, pp. 34-41.
- International Institute of Welding. (2019). Guidelines for Selecting Welding Wire Feeders for Industrial Applications. IIW Document XII-2109-19.
Three Water Machinery Co., Ltd.
Three Water Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of welding wire auxiliary equipment in China. With abundant experience, we warmly welcome you to buy advanced equipment for sale here and get quotation from our factory. Contact us for more details.
Address: No.15, Jiaye Road, Liuanzhuang Industrial Park, Beichen District, Tianjin, China
E-mail: sales@eqet.com
WebSite: https://www.eqet.com/
